Production Scheduling
Kanban Manufacturing: When Visual Flow Improves Production Control
Published November 12th, 2026
Kanban manufacturing uses visible signals to control how work moves and when materials or jobs should be replenished. For manufacturers facing excess work in process, unclear priorities, or frequent schedule changes, kanban can make flow easier to see and manage. It is not a universal replacement for production planning: it works best when the process, replenishment rules, and limits are clear.
Discuss your production planning needs
What does kanban manufacturing mean?
Kanban is a visual pull method. A downstream process signals that it is ready for more work or material, and that signal authorizes replenishment. The signal might be a card, container, marked location, electronic message, or status on a shared display. The medium matters less than the rule it represents: no signal, no replenishment.
In a manufacturing setting, kanban may regulate purchased components, parts moving between operations, or the release of repeat production jobs. A card can identify the item, quantity, source, destination, and replenishment instructions. When a container is emptied or a work step consumes its allotted quantity, the signal returns to the supplying process.
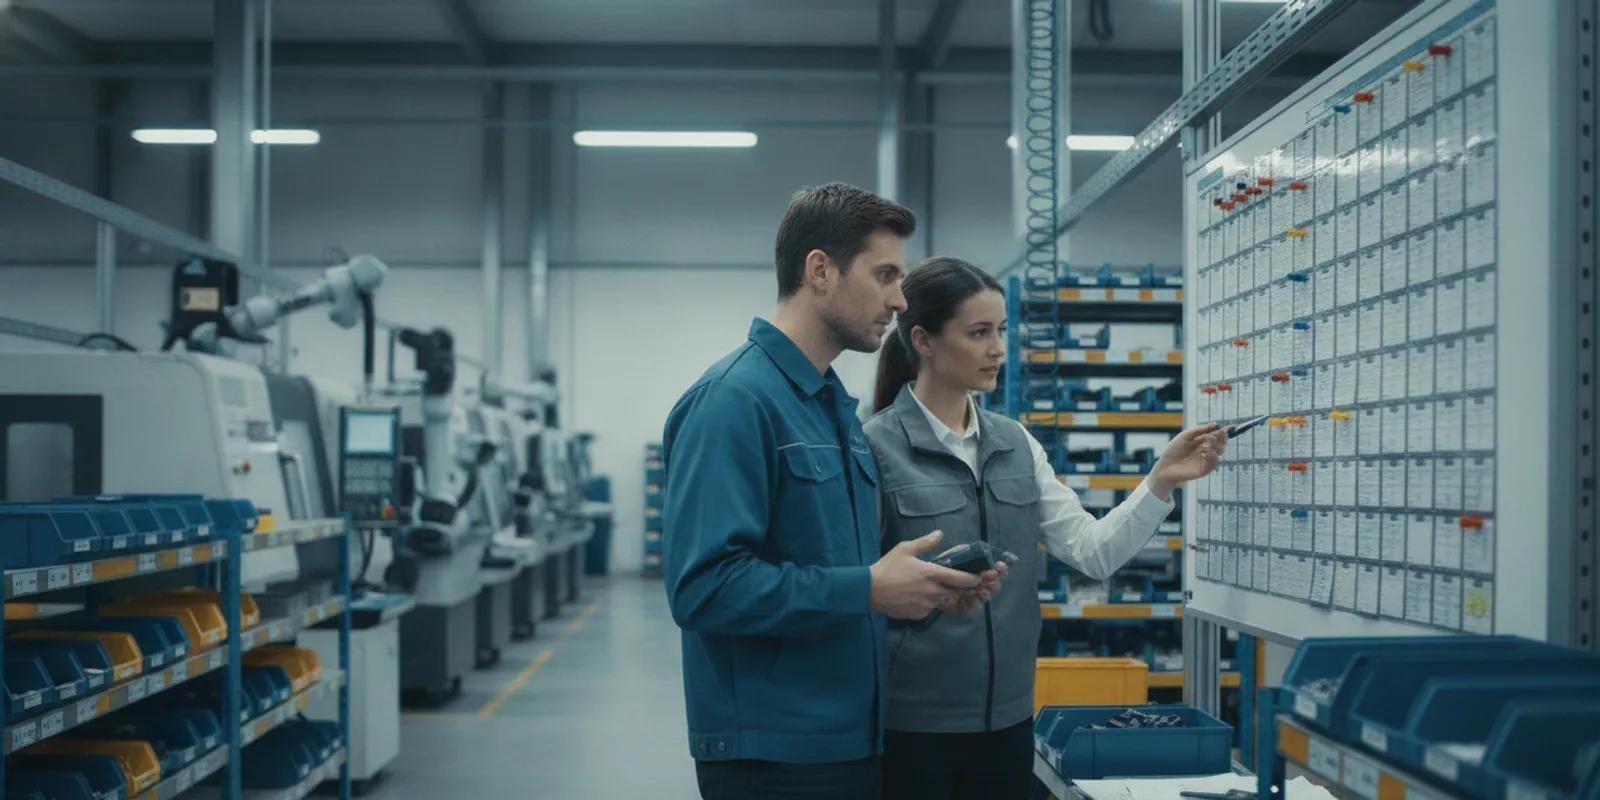
This is different from simply putting a board on the wall. A board may show status without controlling release. A functioning kanban system connects a clear signal to a defined action and a controlled quantity. Teams can see what is waiting, what is authorized, and where replenishment is needed.
Why use visual pull signals?
Without a shared release rule, work often enters a shop because someone has spare capacity, a customer is asking for an update, or a planner is trying to keep every machine busy. That can increase queues without making the whole order move faster. Visual pull gives the team a way to make work-in-process limits visible and tie replenishment to actual consumption.
- More visible priorities: Operators can identify the next authorized task instead of relying on scattered messages.
- Controlled queues: A limit on cards or containers helps prevent uncontrolled accumulation between steps.
- Earlier signals: A depleted buffer or returned card prompts action before a shortage becomes a surprise.
- Clearer coordination: Upstream and downstream teams use the same signal and quantity rather than informal assumptions.
- Better problem visibility: When a queue is empty or a signal is stuck, the team can investigate a specific process issue.
Kanban does not by itself remove a bottleneck, correct inaccurate routings, or make an unreliable process predictable. It makes the relationship between consumption and replenishment easier to manage. The process still needs owners who respond to signals and address recurring causes of delay. For broader process-improvement learning, the American Society for Quality provides resources for quality and continuous improvement practitioners.
Where does kanban fit in a manufacturing operation?
Kanban is especially practical for repeatable work with relatively stable demand and a known replenishment path. Common applications include bought-in fasteners and standard components, replenishment between a machining cell and an assembly area, or repeat parts produced in defined quantities. It may also support a controlled queue between steps where downstream consumption is visible.
It is less straightforward for one-off orders, highly variable routings, long or uncertain setup requirements, or work driven by changing customer priorities. Those conditions do not automatically rule out visual pull, but they make sizing and replenishment rules more difficult. A signal system cannot substitute for knowing which order needs to ship first or whether a machine and qualified operator will be available.
Many manufacturers therefore use a hybrid approach. Kanban can govern stable repeat items or a defined buffer, while finite-capacity scheduling coordinates jobs with due dates, shared equipment, special tooling, or outside processing. A schedule can establish sequence and timing; kanban can make local consumption and replenishment visible. See how production scheduling and shop-floor management can support coordination across operations.
How do you compare kanban with other control methods?
The right method depends on what needs control. A visual card system is not inherently better than a schedule, reorder point, or dispatch list. The comparison below is a starting point; actual design depends on product mix, lead times, constraints, and the quality of shop-floor data.
| Method | Primary signal | Useful when | Watch for |
|---|---|---|---|
| Kanban pull | Consumption or an empty container triggers replenishment | Demand and replenishment are repeatable, and quantities can be controlled | Unclear ownership, poorly sized buffers, or demand swings that outpace replenishment |
| Production schedule | Planned sequence and timing for orders or operations | Due dates, machine capacity, routing, and priorities must be coordinated | Plans need timely updates when actual conditions change |
| Reorder point | Inventory reaching a defined threshold triggers a purchase or make action | Stock usage and replenishment lead time can be estimated | Incorrect records or variable lead times can create shortages or excess stock |
| Manual dispatch list | Supervisor or planner communicates the next work | Low-volume work needs direct judgment and priorities change often | Information can become stale or inconsistent across shifts |
These methods can coexist. For example, a planner may schedule a constrained machine while a two-bin signal replenishes a standard fastener used by several cells. The important thing is to define which method controls which decision. If a kanban signal conflicts with a customer expedite or a capacity constraint, workers need an agreed escalation rule rather than an informal workaround.
A practical way to choose is to name the decision first. Is the team deciding what order should run next, how many standard parts to replenish, or when to buy more stock? A schedule is designed to coordinate time, order, and capacity. A kanban signal authorizes a defined quantity in response to consumption. A reorder point is an inventory threshold. Using a single label for all three decisions obscures who acts and what the signal means.
How should you design a kanban system?
Start with a narrow, observable flow instead of converting the entire plant at once. Select an item or process where consumption can be seen, replenishment can be assigned, and shortages or excess queues are causing a practical problem. Before issuing cards, walk the route with the people who move and use the material. The current method may include informal staging or undocumented checks that the proposed design must account for.
- Map the current flow. Follow the item from its source through storage and each operation to the point of use. Record who handles it, where it waits, how replenishment is requested, and what commonly interrupts the flow.
- Choose a suitable pilot. Prefer repeatable items with a defined source and destination. Avoid beginning with the most volatile, custom, or capacity-constrained work unless the pilot is specifically intended to solve that control problem.
- Set the signal and ownership. Decide what event creates a signal, who receives it, who replenishes, and how completion is confirmed. Make responsibilities clear across shifts.
- Define the quantity and limit. Establish how much each signal authorizes and how many signals may be active. The limit should reflect actual usage and replenishment conditions, not a desire to keep every station full.
- Make the rules visible. Put the item identity, quantity, source, destination, and response instructions on the card or display. Use consistent locations and status conventions that workers can understand at a glance.
- Test the exceptions. Agree what happens when stock is missing, a card is lost, a machine is down, quality holds a lot, or demand changes. A controlled exception process is better than quietly creating duplicate signals.
- Review and adjust. Observe the pilot through real replenishment cycles. Compare the intended rule with what workers actually do, then change quantities, placement, or escalation steps based on evidence.
Use actual usage and replenishment experience to set initial limits. A simple conceptual estimate for the number of containers is demand during replenishment lead time divided by container quantity, with an allowance for known variation. This is a starting estimate, not a universal formula: lead time may include queueing, transport, inspection, setup, or supplier delay. Validate the result against real conditions and monitor whether the buffer is repeatedly empty or consistently overfull.
For example, suppose a cell consumes a standard component at a steady pace during a shift, and the supplying area takes a known interval to replenish a tote. Estimate how many units are used during that interval, divide by the tote quantity, and compare the result with observed variability. If the calculation suggests a fraction of a tote, round in a way that respects the actual container size and then test it. Do not treat the arithmetic as proof that the process is stable. A sudden rush order, a supplier delay, or a long setup can change the situation.
What information should each signal contain?
A signal should enable action without requiring workers to search through unrelated paperwork. For a physical card, include only the information needed to identify and move the work accurately. For an electronic signal, make the same details accessible where the decision is made.
- Part or material identifier and a plain description.
- Standard quantity authorized by the signal.
- Supplying location and destination or point of use.
- Replenishment instruction, including any handling or inspection step that matters.
- Signal identifier or status so duplicate and missing cards can be identified.
- Escalation route for shortages, quality holds, and exceptions.
Keep the signal synchronized with the item and its actual route. If a part changes location, pack quantity, or approved source, update the relevant instructions and remove obsolete cards. A signal that looks authoritative but describes an outdated process creates confusion rather than control.
Physical design matters too. A card that is hard to read, easy to detach accidentally, or stored far from the point of use can undermine a sound rule. Choose a consistent return location and make the replenishment state visually distinct from a completed move. If the signal is electronic, ensure the person responsible can see it at the time they need to act; a notification buried in an inbox is not a useful control.
How do you set limits without creating new problems?
A limit should restrain unnecessary work while protecting the process from ordinary replenishment variation. Set it too high and the system may simply relabel excess inventory as a buffer. Set it too low and normal delays can starve the next operation. The best limit is reviewed in context rather than treated as a permanent number.
Look at consumption patterns, replenishment time, batch or container size, process reliability, and the consequence of a shortage. If demand changes materially, a quantity based on old usage may no longer fit. If the replenishment process is erratic, adding containers can conceal the underlying problem. Investigate the cause as well as deciding whether a temporary buffer adjustment is justified.
Track the reason for each exception. A recurring shortage may point to long changeovers, delayed material movement, quality holds, inaccurate inventory, or a supplier issue. The signal can identify where flow broke down, but improvement requires addressing the process condition behind it. Record whether the exception was a one-time event or a repeat pattern and who owns the follow-up.
When adjusting a limit, make the change deliberate and visible. Note what evidence prompted it, who approved it, and when the team will review the new setting. Otherwise, temporary additions tend to become permanent without anyone checking whether the original cause was fixed. A useful review asks both whether the process had enough material and whether the revised limit created extra stock or work elsewhere.
What should you measure during a pilot?
Choose a small set of measures that answer whether the method improves control without shifting the problem elsewhere. Compare a baseline with the pilot period, and record changes in product mix, staffing, or customer demand that make a direct comparison less meaningful.
- Shortages at point of use: How often does the process lack the item when needed, and why?
- Work in process: Are queues and container quantities staying within the agreed limits?
- Replenishment response: How long does it take from signal to replenishment, and how variable is that time?
- Schedule performance: Does the new local control support or interfere with planned order priorities?
- Expedites and workarounds: Are emergency requests, duplicate cards, or untracked moves increasing?
- Usability: Can employees across shifts interpret the signal and follow the same process?
Define each measure before the pilot so the team collects information consistently. For a shortage measure, decide whether a missed pick, a delayed operation, and a line stop are counted separately or together. For replenishment response, agree whether the clock begins when the signal is created, received, or accepted by the supplying area. A few clear definitions are more useful than a large dashboard of ambiguous numbers.
These measures help a team decide whether to retain, adjust, or stop a pilot. They are not a guarantee of a particular performance result. Record the specific operational objective at the outset, such as fewer point-of-use shortages or a more controlled queue, and judge the method against that objective. Also look for side effects: a local buffer may improve availability while increasing storage needs or hiding a delay upstream.
What are common kanban implementation mistakes?
- Launching too broadly. A plant-wide rollout makes it harder to find defects in the rules. Start with a manageable flow, learn, and then extend only where the method fits.
- Adding cards without addressing lead time. More authorized work may hide delays while increasing inventory. Understand what replenishment actually takes before increasing the limit.
- Using signals without ownership. A card is not useful if no role is accountable for responding and confirming replenishment.
- Mixing control systems without precedence. If the schedule, a kanban card, and a supervisor’s request give different instructions, define which governs and how exceptions are resolved.
- Ignoring data quality. Incorrect item identities, locations, quantities, and routings undermine the signal. Verify the underlying records and physical labels.
- Treating compliance as the goal. The objective is reliable flow and clearer control, not simply having every card in its proper place. Ask whether the system helps employees act and exposes process issues.
Also plan for training and shift handoffs. Explain the purpose of the limits, what counts as a valid signal, and where to raise exceptions. Invite operators to identify confusing steps; they see the real movement of work and can spot gaps that a desk-based design may miss.
A small tabletop walkthrough can reveal gaps before a live trial. Give the team a sample card and ask them to describe what happens when the bin empties, when the source is short, and when a lot is placed on hold. If different shifts give different answers, clarify the rule before launch. Include a plan for replacing damaged cards and reconciling missing signals so workers are not tempted to create unauthorized duplicates.
How can digital tools support visual flow?
Physical cards and marked locations can be effective when the flow is local and easy to observe. As work crosses departments or involves many jobs, a digital view may help planners and supervisors see status and coordinate priorities. Digital tools do not make poor rules better; the process and signal logic still need to be defined.
Useful shop-floor information can connect operational status with planned work, helping teams understand what is moving, waiting, or at risk. A manufacturer evaluating software should ask how it handles current ERP data, routings, work queues, and exceptions, and whether the people making decisions can access the information they need. JobPack describes its production scheduling and machine monitoring solutions as tools for visibility and coordination across manufacturing operations.
For a broader look at how execution systems relate to planning tools, see this guide to ERP, MES, and APS. The aim is not to digitize every card automatically. First decide what information is valuable, who acts on it, and how it should connect to the schedule and inventory records.
When reviewing a digital option, walk through real scenarios rather than only a polished demonstration. Ask how an operator sees the authorized job, how a planner learns that a machine is unavailable, and how a supervisor records a quality hold. Clarify which system is the source of truth for item quantities and routings. If a digital board and a physical card can disagree, define how the mismatch is resolved and which record is corrected.
How should you decide whether kanban is a fit?
Ask a few practical questions before committing to a rollout:
- Is the item or work repeatable enough that consumption can trigger replenishment?
- Can the supplying process respond within a known and acceptable time?
- Can the team define an appropriate quantity and enforce a visible limit?
- Are item records, locations, and routes reliable enough to support the signal?
- Will planners and operators know how to resolve conflicts with due dates, machine capacity, or urgent work?
- Can the pilot be measured and reviewed by the people responsible for the process?
If the answers are mostly yes, a limited pilot can test whether visual pull improves control. If not, work on process stability, inventory accuracy, routing clarity, or capacity planning first. For variable, order-driven work, a production schedule may remain the primary control, with kanban reserved for stable materials or repeat flows.
Consider a shop that makes custom assemblies but uses the same standard fastener across many orders. The assembly sequence changes with due dates and machine availability, so a schedule is needed to coordinate jobs. Yet the fastener has a stable source, known tote size, and visible consumption. A kanban signal can replenish that item without trying to make every custom job follow the same pull rule. This division of responsibility keeps the method focused on the decision it can manage well.
Request a production scheduling demo
Frequently asked questions
Is kanban the same as just-in-time manufacturing?
No. Kanban is a signaling and replenishment method that can support pull-based production. Just-in-time is a broader operating aim of making or supplying what is needed when it is needed. A card system alone does not ensure that a process is reliable or that replenishment arrives on time.
Can a job shop use kanban?
Yes, in selected areas. A job shop may use kanban for repeat components, standard supplies, or a stable buffer between operations, while using capacity-aware scheduling to manage custom orders, changing due dates, and shared machines. The fit depends on the repeatability of the particular flow.
How many kanban cards should a process have?
There is no single correct number. Estimate demand during the actual replenishment time and account for container quantity and known variation, then test the result. Review shortages, excess stock, and changing demand rather than keeping an initial estimate indefinitely.
Do kanban systems have to be digital?
No. Cards, containers, and marked locations can provide a clear signal for a simple, local process. Digital support may be useful when status must be shared across teams or connected to scheduling and inventory information, but it should reflect defined working rules.
Make flow visible, then refine the rules
Kanban manufacturing is most useful when a visible signal connects consumption to an owned replenishment action and a controlled quantity. Start where work is repeatable, define how exceptions are handled, and use the pilot to learn whether the limits and response times fit reality. Where jobs, capacity, and priorities vary, combine local pull signals with clear production scheduling rather than expecting one method to control every decision. For a practical conversation about connecting shop-floor control with scheduling, contact JobPack.
A well-designed visual system should make the next action clearer and help the team see where flow needs attention.