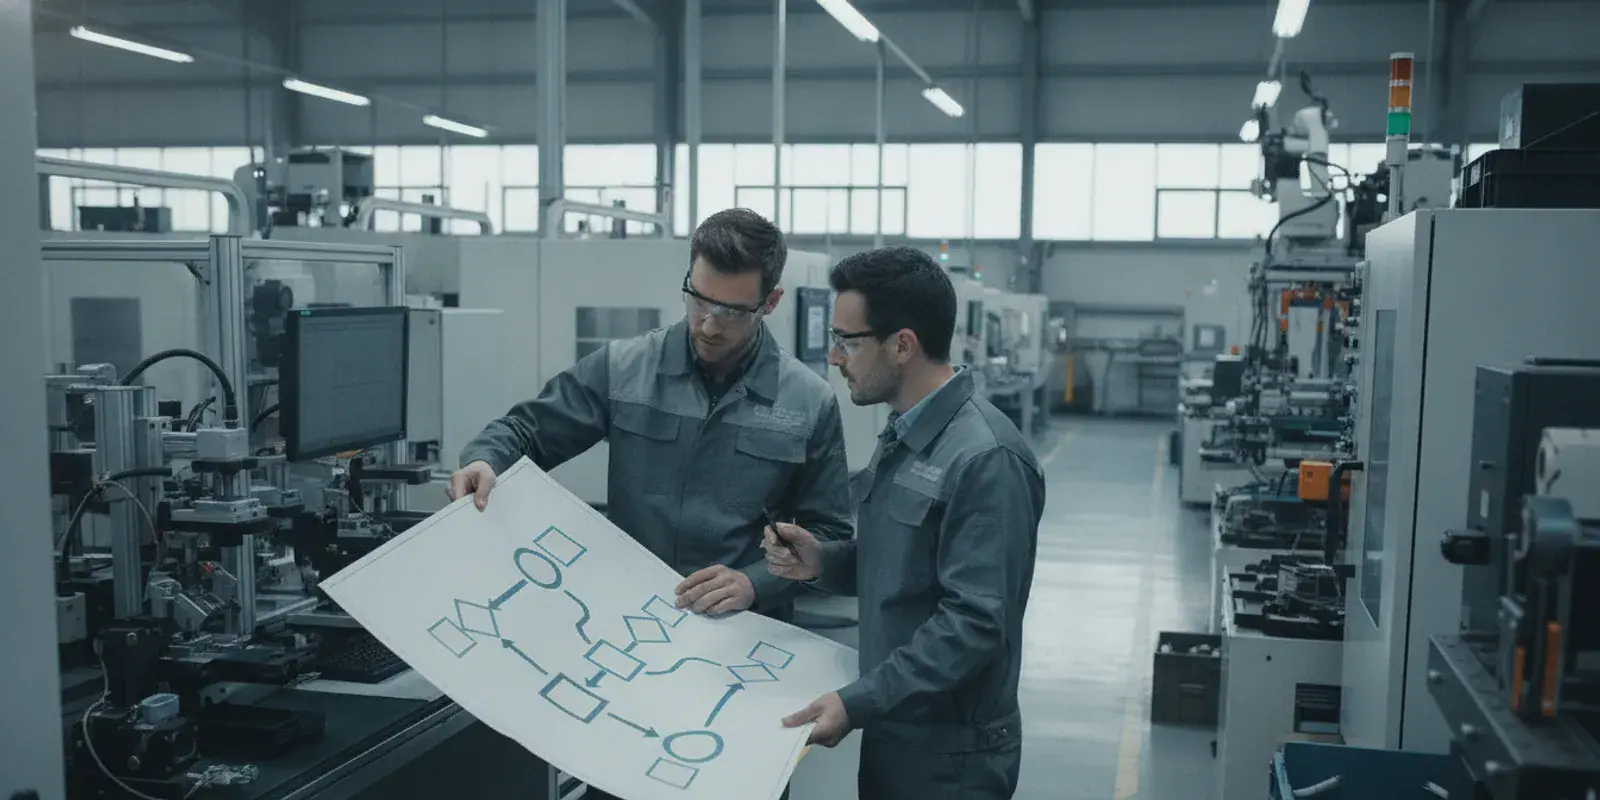
Value stream mapping examples manufacturing teams can use make queues, delays, and information gaps visible across a product family. A value stream map links customer demand, production steps, material movement, and the information that directs work. The examples in this guide show how to choose a useful scope, record the current process, and turn evidence into a practical improvement test.
Talk with JobPack about production planning
What does a value stream map show?
A value stream map (VSM) represents the activities required to deliver a product or product family, from incoming material through shipment. It distinguishes processing from waiting, marks inventory or work-in-process (WIP), and shows information flow: who releases orders, how priorities are sent, and how production status reaches planners. A map can cover a physical production route, the decisions that control that route, or both.
Teams usually begin with a current-state map based on observation and operating data. They then draw a future state that represents a better flow under stated assumptions. The purpose is not to produce a polished diagram or to remove every buffer. It is to agree on what happens, locate a specific point of friction, and test a change without treating an unverified assumption as fact. For background on lean principles that inform this kind of process improvement, see the Lean Enterprise Institute, a nonprofit organization focused on lean practice.
For example, a process may require only a few hours of hands-on work but several days from release to shipment. The map helps the team ask where that elapsed time is spent: waiting for a machine, a decision, a component, a quality check, or an outside supplier. Each cause suggests a different response. A longer queue at inspection calls for a different investigation than missing material or unclear order priorities.
How should you choose a process to map?
Choose a product family that shares a sufficiently similar route. Mapping every product and department at once can make the result too broad to use. Routing records and order history can help identify a family, but confirm the common steps with the people who run the process. If important routes differ, split them into separate maps or show the variation clearly.
- Set the boundary. State where the map begins and ends, such as supplier receipt to shipment, or approved work-order release to completion.
- Select a representative family. Include a recurring route and record exceptions instead of hiding them. Avoid selecting only the smoothest or most troublesome order unless that is the explicit question.
- Involve people doing the work. Operators, planners, material handlers, inspectors, purchasing staff, and supervisors can explain actual handoffs.
- Choose consistent units. Define the period and units for demand, queue counts, processing time, and observations.
- Name the reader and decision. Decide whether the map will help explain late orders, excess WIP, missed handoffs, or another bounded problem.
- Check whether the scope is answerable. Confirm that the team can observe the work and obtain enough data to assess a possible test.
A practical scope statement might read: “This map follows family A from approved work-order release through final inspection, using orders completed during the last four weeks.” The exact period should fit the process and the question. A short period may miss a monthly demand pattern; a long period may combine operating conditions that have since changed. State what was included and what was excluded, so another person can understand the map without guessing.
A useful selection exercise is to list candidate families and compare their route similarity, frequency, current operational concern, and data availability. If a family has three common routes but one accounts for most orders, map that route first and mark the others as exceptions. If the routes are equally common and have different constraints, separate maps may be easier to validate. This is a scoping decision, not a claim that all products can be grouped neatly.
What information belongs on the current-state map?
Walk the process from the customer end back toward the beginning, then verify the sequence with the people doing the work. Record both physical movement and the information that triggers it. Work instructions and routings are useful context, but the map should represent how work actually runs, including rework loops, queues, and informal priority changes.
- Demand pattern or order cadence relevant to the family and period.
- Each production and inspection step, with observed processing time and changeover information where available.
- Queue or inventory quantities between steps, together with observation date and counting method.
- Material movement, outside processing, and transport when these affect flow.
- Order release, priority updates, status reporting, and the people responsible for each handoff.
- Known constraints, quality checks, rework, holds, route exceptions, and the conditions that trigger them.
- How work is sequenced, including whether a step follows a dispatch list, planner instruction, physical signal, or another method.
Separate observations from estimates. If a queue count is a snapshot, label it as one. If processing time varies by shift, order, or product, note a range or the source rather than presenting one reading as universal. A simple data note can record the step, value, unit, date, source, and whether the value is measured or estimated. If two people count a queue differently, agree on a counting rule before comparing numbers.
Do not confuse processing time with elapsed lead time. A machine may work on a part for a short interval while the job waits much longer. Both matter, but they answer different questions. Likewise, a buffer may protect a downstream process from variation; its presence alone does not prove it should be removed. Record why the buffer exists if that is known, and mark the reason as a hypothesis if it has not been verified.
Information flow deserves the same care as material flow. Note who creates a due date, how a revision reaches the floor, and how an operator reports a completed operation or a delay. A map that shows machines but omits the release and update rules can misdiagnose a scheduling problem as a capacity issue. For an adjacent discussion of shop-floor WIP tracking, consider how work status and queue visibility are represented in the process.
What are practical value stream mapping examples in manufacturing?
1. High-mix job shop with shared machines
A job shop may route custom parts through cutting, machining, inspection, and outside processing. Some jobs revisit a resource, while others take different paths. Map one family or representative route, then mark where jobs wait for a shared machine, an inspection decision, or a priority change. Include the order release process and any routing variation that changes the route materially.
Suppose a hypothetical team sees machined jobs accumulating before inspection. That observation does not establish the cause. The team checks whether inspection capacity, missing paperwork, a batch policy, or shifting priorities explains the queue. It records the time a representative order completes machining, becomes ready for inspection, enters the queue, and receives a disposition. These timestamps can reveal whether the reported delay is actually a queue or a wait for information.
A first test might define a consistent inspection handoff: the required paperwork travels with each job, and a named role confirms readiness at a specified point in the shift. The team can compare queue counts and elapsed time for the same family before and during the test. It should also note order mix, staffing, and unusual machine interruptions. If the mix changed substantially, an apparent improvement may not be attributable to the handoff change. The result may show that the hypothesis was wrong; that is useful evidence for the next investigation.
2. Repetitive production line
For a stable product family, show each station, cycle time, changeovers, buffers, and replenishment signals. Compare the observed pace at each step with the demand rate for the period studied. A buffer that repeatedly grows in front of one operation may point to uneven work, interruptions, a quality hold, or a release policy that sends work faster than the next step can process.
Imagine that the map shows a recurring accumulation before a finishing station, while the operation after finishing is often waiting. First check how the observations were taken: are both counts from the same shift boundary, and do they cover the same products? Then examine whether finishing has longer changeovers, a different staffing pattern, rework, or material replenishment delays. A single snapshot cannot distinguish these possibilities.
A possible experiment is to adjust release quantities, balance a portion of work between stations, or clarify the replenishment signal. Before changing a buffer, ask what risk it protects against: long replenishment time, reliability variation, quality holds, or another condition. The future-state map should show the intended change and any control needed to protect delivery. A team might also track the queue at the constraint and the next operation’s waiting time, rather than relying on a general impression that the line “looks better.”
3. Make-to-order assembly with purchased components
Assembly can look productive at the workstation while orders wait for missing components or engineering clarification. Map order entry and release alongside purchasing, receiving, kitting, assembly, and final inspection. Note when information is created, who owns it, and how a change reaches the floor. A revision or substitute component can alter readiness even when the original work order was released on time.
If orders are released before kits are complete, test a readiness check or a different release trigger. If drawings change after release, clarify revision control and the point at which the shop receives approved information. Track incomplete kits, holds, and elapsed time across the chosen boundary. A readiness rule should be tested against real constraints; it may reduce avoidable starts but cannot make a supplier deliver a missing component sooner.
For a concrete hypothetical case, select a small group of comparable orders. At release, record whether each kit is complete, whether current approved instructions are available, and any known exception. At assembly start, record the remaining shortages and the time spent waiting for clarification. Review the exceptions with purchasing, engineering, and production rather than labeling every incomplete order a planning failure. The map can then distinguish a material-availability issue from a document-control or release-rule issue.
4. Outside processing and return-to-shop flow
Heat treatment, coating, plating, or another external operation introduces transport and a handoff beyond the facility. Map dispatch, supplier processing, expected return, receipt, and the next internal step. Record how dates and status are exchanged, and where material waits before dispatch and after return. If several outside operations are involved, clarify whether the map follows one route or a family with alternatives.
The main uncertainty may not be supplier processing time. It could be the time between a status change and the planner learning about it, or the time a returned lot waits for receiving inspection. A team might test a standard update cadence, a clear follow-up owner, or an escalation point. Compare the same measures over a representative period, noting supplier and product variation. Do not combine supplier lead time, transit time, and internal waiting into one number if the goal is to find which part of the handoff needs attention.
5. Rework loop after an inspection finding
A process map can also make a rework loop visible. For a recurring product family, show the inspection decision, the route back to an earlier operation, any required authorization, and the return to inspection. Record the reason codes or descriptions that already exist, but avoid inventing a cause when the records are incomplete. The loop may consume capacity in multiple departments and can affect other jobs even when the reworked part is only a small share of the queue.
For instance, a hypothetical map might show that a job waits for a disposition before rework can begin, then joins the normal queue again. The team can separate wait for disposition from rework processing and subsequent waiting. A possible test may clarify who owns a disposition request and how its status is communicated. It should not bypass the required quality decision. The point is to examine the whole loop and preserve necessary inspection and authorization controls.
| Manufacturing example | Flow to include | Question to verify | Possible first test |
|---|---|---|---|
| High-mix job shop | Work-order release through shared resources and inspection | Where do queues or priority changes arise? | Define and check a consistent handoff routine |
| Repetitive line | Stations, buffers, changeovers, and replenishment signals | Which step repeatedly accumulates work, and why? | Test a release quantity or station-balance change |
| Make-to-order assembly | Order release through purchasing, kitting, and inspection | Are kits and approved instructions ready? | Test a readiness check before release |
| Outside processing | Dispatch, supplier step, return, and next operation | Who owns status visibility and follow-up? | Test a status cadence and assigned owner |
| Rework loop | Inspection finding, disposition, rework, and reinspection | Where does the part wait, and what controls apply? | Clarify the request owner and status handoff |
How can you compare current and future states?
A current-state map describes what the team observed. A future-state map describes a proposed way of working. Keep the distinction visible and write down assumptions behind the proposal. The future state should not simply erase queues or compress every time value; it needs to explain how work will flow and what safeguards will remain.
Use a comparison table or action register to make the proposal concrete. For each change, name the process point, present condition, intended condition, and evidence that would indicate whether the change helped. If jobs wait for a missing kit, the current condition might be “orders released with components outstanding.” The proposed condition might be “release after a documented readiness check,” with incomplete-kit counts and elapsed time as review measures.
Draw the information flow as carefully as the material flow. If the future state depends on a person seeing a status update, specify who receives it, when, and what action follows. If it depends on a system record, identify the required data and its owner. A line on a diagram is not a working control until someone knows what to do when the expected signal is absent. State what happens to an urgent exception rather than assuming every order follows the standard route.
A useful comparison separates the expected benefit from the conditions required to achieve it. For example, moving from large releases to smaller releases might reduce queue accumulation, but only if setups, material replenishment, and dispatch rules can support that pattern. If any condition is uncertain, identify it as a question to test. A future-state map is a working proposal, not a promise that a target time or result will be achieved.
How do you turn a map into an improvement plan?
A map is a diagnostic aid, not proof that a particular solution is needed. Select one observed problem and state it in a testable way: what happens, where, for which family, and why it matters. Then choose a bounded change that can be evaluated without putting customer commitments at risk.
- Set a baseline. Choose measures that fit the issue: queue quantity, time between steps, incomplete kits, late status updates, or schedule changes. Define counting rules, units, and the review period.
- Check the suspected cause. Ask people closest to the work and distinguish confirmed observations from hypotheses. Check whether the same pattern appears across more than one order or shift.
- Design a small test. State the change, scope, owner, start date, and what should happen if an exception occurs. Keep current safety, quality, and customer controls in place.
- Draw the future state. Show intended flow, information signals, necessary buffers, and controls. Mark assumptions that need validation.
- Review comparable evidence. Compare with the baseline and note differences in product mix, demand, staffing, or equipment availability.
- Decide what to do next. Keep, adjust, or stop the change based on what evidence supports, then update the map.
A short action register can keep the work moving. For each item, record map location, observed condition, hypothesis, action owner, measure, due date, and review date. A usable entry might read: “Inspection queue: determine whether jobs are waiting for paperwork; owner: inspection supervisor; measure: ready-to-inspect queue at shift end and time from readiness to disposition; review: after two weeks.” That gives the team a specific question and observable evidence, unlike a broad note such as “improve inspection.”
Choose a measure that cannot be improved by shifting the problem elsewhere. If a release change reduces the queue at one station but increases incomplete kits downstream, review both. If the measure is a time interval, define its start and end events. If the measure is a count, specify which orders or parts qualify. Consistent definitions matter more than adding a long list of metrics that no one can maintain.
Where a change could affect safety, quality, or customer requirements, include the appropriate review before testing. A flow improvement should not bypass a required inspection or release decision. The team can still simplify a handoff, improve visibility, or remove avoidable waiting while preserving necessary controls. Assign a person to pause or escalate the test if an exception threatens those controls.
How can scheduling and shop-floor information support a map?
Value stream mapping highlights where flow and information interact. If planners cannot see whether an operation has started, whether a machine is available, or whether a job is waiting for a decision, the map may expose a visibility gap. First decide what information is needed, how often it changes, and who will act on it. A schedule should reflect actual constraints and route details, not a theoretical sequence alone.
For context on how planning tools fit the production process, see JobPack’s production scheduling solution. Mapping can clarify what the schedule needs to represent, such as operation sequence, due-date priorities, or a status update. It does not, by itself, establish that a software change is required. Teams can also review how ERP, MES, and APS differ before deciding which process or system deserves attention.
Other useful background includes MES implementation planning, the meaning of OEE, and WIP analysis. These are adjacent topics, not a required checklist for every mapping effort. Choose measures that fit the process rather than adding every available metric to one project. A team studying an information handoff may need to clarify who receives a status signal before it needs a machine metric.
Before selecting or changing a tool, write down the work the tool must support. For example: “When an operation is reported complete, the next eligible step should be visible to the planner, and the status should identify the reporting time.” Then check whether that need is met by the current process, an existing system, or a proposed change. This sequence keeps the map focused on the operating question rather than on a feature list.
What mistakes make a value stream map less useful?
- Mapping the ideal instead of the actual process. Observe work and include informal routes, delays, and rework.
- Choosing a scope that is too broad. Split distinct families or routes into maps people can verify.
- Presenting estimates as measurements. Label data sources, collection dates, and variation.
- Calling every non-processing step waste. Some checks and approvals may be necessary for quality, compliance, or customer requirements.
- Removing buffers without checking risk. Find out what variation or supply condition the buffer protects against.
- Jumping straight to software. Define the process problem and information need first.
- Using averages without context. Averages can obscure a long wait or a route exception; include ranges or case details when they change the decision.
- Failing to follow up. Assign owners and review dates, then update the map as the process changes.
Another common problem is collecting more detail than the team can use. A map crowded with every data point can obscure the route and handoffs. Keep the main map readable, and place supporting measurements or exceptions in a separate register. The goal is a shared view that guides a decision, not a complete database of the factory.
It is also easy to treat one map as a permanent description. A change in product mix, routing, equipment, or release rules can make the old picture misleading. Date the map, name its scope, and state when it should be revisited. If the process is changing quickly, a short review after the test may be more useful than waiting for a fixed annual cycle.
Frequently asked questions
How many products should one value stream map cover?
There is no universal number. Group products only when they share a sufficiently similar route and flow. If important steps, constraints, or information handoffs differ, split the family or mark the variation clearly. The map should remain specific enough that the team can verify the observations and act on them.
Should a value stream map include suppliers?
Include supplier steps when they affect the boundary being studied, such as material availability or outside processing. Make the boundary explicit so readers can distinguish internal steps from external handoffs. A map may include the supplier interface and status exchange without claiming to describe the supplier’s internal process.
How often should a map be updated?
Update it when the process, product mix, route, or information flow changes enough to make the map misleading. A periodic review can also help, with the interval set to match the pace of change and the map’s purpose. After a test, record what actually changed and whether the future-state assumptions held.
Does value stream mapping require specialized software?
No. A clear hand-drawn or digital diagram and verified observations are enough to begin. Software may later help maintain data or share status, but it cannot substitute for agreeing on the process and checking the facts. Choose a format that the people who own the process can review and update.
Should a team map the whole factory at once?
Usually, a bounded product family or process is easier to observe and discuss. Start with the question the team needs to answer, then define a beginning and end that capture the important handoffs. If a local issue depends on an upstream or downstream process, expand the boundary deliberately and explain why.
Request a production scheduling demonstration
A useful value stream map turns what a team observes into a focused improvement test, with clear measures and ownership. Start with one product family, verify its current flow, and revisit the map when evidence shows what to change next.