Data Analytics
What is a Manufacturing Execution System? A Simple Guide
Published February 11th, 2026
Your shop floor generates a massive amount of data every single day. From machine cycle times to operator inputs and quality checks, the information is all there. The problem is that it’s often scattered, delayed, or stuck in spreadsheets, making it nearly impossible to use for immediate decision-making. You’re left managing today’s problems with yesterday’s information. A manufacturing execution system (MES) changes that by capturing, organizing, and contextualizing all that data in real time. It transforms a flood of raw numbers into a clear, live picture of your operations, giving you the actionable insights you need to spot bottlenecks and improve efficiency on the fly.
Key Takeaways
- Connect Your Business Plan to Your Shop Floor: An MES acts as the critical translator between your ERP and your machines, turning high-level orders into detailed production tasks and sending real-time performance data back to ensure your business goals and factory operations are perfectly aligned.
- Make Proactive Decisions with Live Data: An MES provides a real-time view of your entire production process, from machine status to quality checks. This immediate visibility helps you solve problems as they happen, reduce waste, and improve efficiency based on accurate, up-to-the-minute information.
- Prioritize Partnership and Planning for Implementation: The right MES is about finding the best fit for your team and processes, not just the most features. A successful rollout involves clearly defining your needs, choosing a supportive vendor, and involving your team in a phased approach to ensure smooth adoption.
What Is a Manufacturing Execution System (MES)?
If you’ve ever felt like there’s a disconnect between your business plans and what’s actually happening on the shop floor, you’re not alone. A Manufacturing Execution System (MES) is designed to solve that exact problem. Think of it as the central nervous system for your manufacturing operations, giving you a clear, real-time window into every process. It’s the bridge that connects your high-level business goals with the day-to-day work of making things. An MES gets your people, machines, and systems on the same page, helping you turn plans into high-quality products efficiently.
What It Is and What It Does
At its core, a Manufacturing Execution System is software that monitors and manages the entire production lifecycle, from the moment raw materials arrive to when finished goods are ready to ship. It tracks every step, collecting data directly from the shop floor to create a complete “as-built” record of your products. This isn’t just about watching processes from afar; it’s about understanding what’s happening right now so you can make smart, immediate decisions. The system helps you improve production efficiency, maintain quality standards, and ensure full traceability for every item that leaves your facility.
How MES Connects Your ERP to the Shop Floor
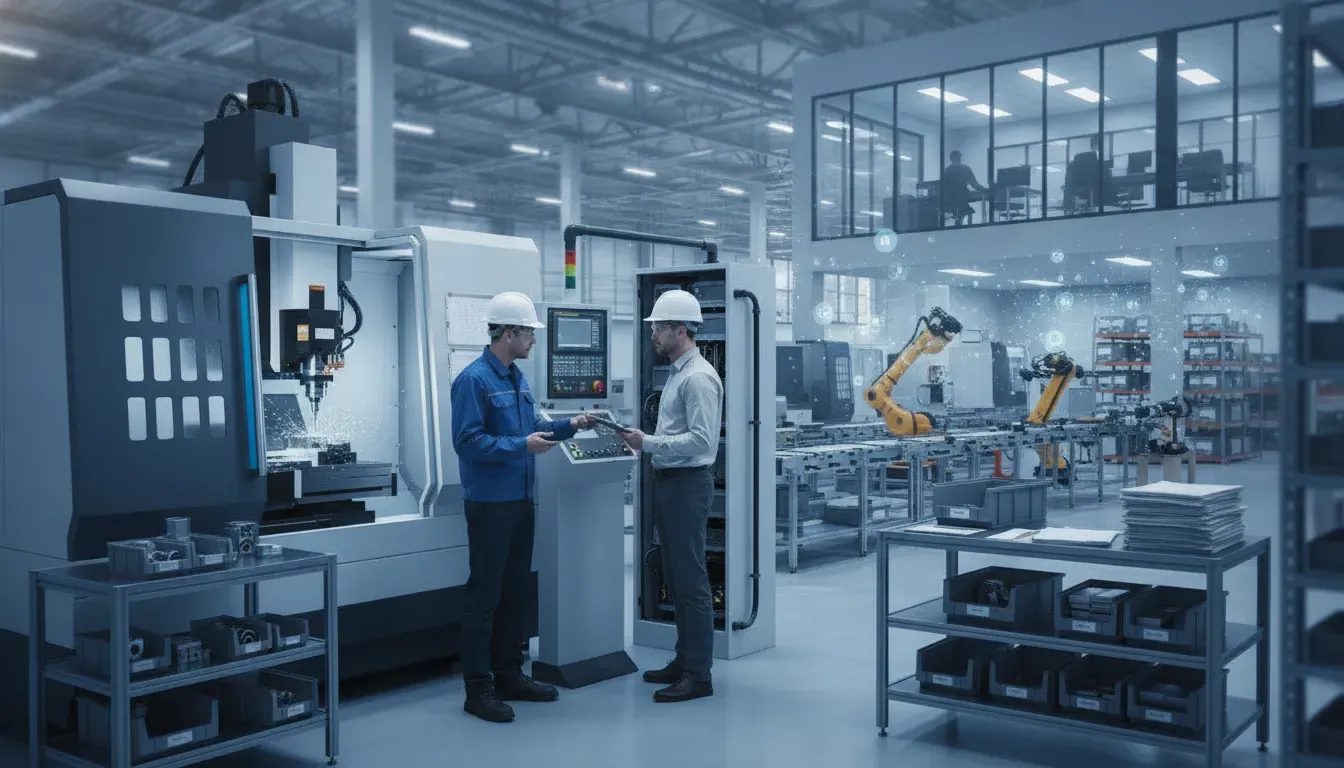
Your Enterprise Resource Planning (ERP) system is fantastic at managing the business side of things—orders, finances, and high-level planning. But it doesn’t speak the language of the shop floor. That’s where the MES comes in. It acts as a vital translator, taking production orders from the ERP and breaking them down into detailed tasks for your machines and operators. As work gets done, the MES feeds real-time production data—like cycle times, material consumption, and quality checks—back to the ERP. This creates a seamless information loop, ensuring your business plans are perfectly in sync with your factory’s actual shop floor data collection capabilities.
What Can an MES Actually Do?
So, what does a Manufacturing Execution System do on a day-to-day basis? Think of it as the central nervous system for your shop floor, connecting your high-level plans to the actual work being done. It’s the bridge between your ERP system and your machines, translating business goals into actionable tasks and sending real-time results back up the chain. An MES isn’t just about collecting data; it’s about using that data to actively manage, control, and optimize every step of the production process. From the moment raw materials arrive to the second a finished product is ready to ship, the MES is involved, ensuring everything runs smoothly, efficiently, and according to plan. Let’s break down its core functions.
Track and Monitor Production in Real-Time
An MES gives you a live, transparent view of your entire shop floor. It tracks the journey of raw materials as they become finished goods, capturing data at every step. This means you can see exactly what’s happening, where it’s happening, and when. Is a machine down? Is a job running behind schedule? You’ll know instantly, not hours or days later. This level of visibility allows you to spot bottlenecks, address issues before they escalate, and make informed decisions on the fly. With effective machine monitoring, you can move from reactive problem-solving to proactive process improvement, ensuring production stays on track.
Manage Work Orders Seamlessly
Forget shuffling paper trails and manually updating spreadsheets. An MES digitizes and automates your work order management. It receives orders from your ERP system and dispatches them to the correct workstations on the floor. The system ensures that operators have all the necessary information—like instructions, specs, and material requirements—right at their fingertips. If priorities shift or an unexpected issue arises, the MES can dynamically adjust schedules and reroute work orders to keep production flowing. This creates a more agile and responsive manufacturing environment where everyone is working from the same, up-to-the-minute playbook.
Schedule and Allocate Resources
One of the most powerful functions of an MES is its ability to optimize your production schedule. It goes beyond simple planning by considering real-world constraints like machine availability, tool readiness, material supply, and labor skills. The system helps you create realistic and efficient schedules that maximize throughput and minimize idle time. By intelligently allocating resources, an MES ensures that the right people and equipment are working on the right jobs at the right time. This strategic approach to production scheduling is fundamental to meeting deadlines, controlling costs, and keeping your customers happy.
Maintain Quality Control and Compliance
Quality isn’t just about inspecting a product at the end of the line; it’s about building it into every step of the process. An MES helps you do just that by enforcing quality checks and procedures throughout production. It can prompt operators to perform specific tests, record measurements, and verify standards at critical points. If a part or process falls out of spec, the system can flag it immediately, preventing defective products from moving forward. This is especially vital for industries with strict regulatory requirements, as the MES creates a detailed digital record for compliance and audits.
Manage Inventory and Trace Products
An MES provides precise, real-time tracking of your inventory, from raw materials to work-in-progress (WIP) and finished goods. By integrating with your shop floor data collection processes, it knows exactly what materials have been consumed for each job, reducing the risk of stockouts and minimizing excess inventory. Furthermore, it creates a complete genealogy for every product you make. This end-to-end traceability means you can track every component and process associated with a specific unit or batch. In the event of a recall or quality issue, you can quickly identify the affected products, saving significant time and resources.
How MES Works with Your Other Systems
An MES isn’t a standalone tool that you just plug in and forget. Its real strength comes from its ability to communicate and integrate with the other software and hardware you already use. Think of it as the central nervous system of your shop floor, connecting the brain (your business planning) to the hands (your machines and operators). This seamless integration creates a single, unified view of your entire manufacturing process, from the top floor to the shop floor. By linking these systems, an MES ensures that everyone and everything is working from the same, up-to-the-minute information, which is crucial for making smart, timely decisions.
Connecting with Your ERP
Your Enterprise Resource Planning (ERP) system is great at managing the big picture—things like customer orders, overall inventory, and finances. But it doesn’t have visibility into the real-time specifics of what’s happening on the factory floor. That’s where the MES comes in. It acts as a vital bridge, translating high-level production plans from the ERP into detailed, actionable tasks for your shop floor team. As work is completed, the MES feeds crucial data—like material consumption, labor hours, and production counts—back to the ERP. This two-way communication keeps your business data accurate and ensures your production scheduling is always aligned with your business goals.
Linking to SCADA and IoT Devices
While the ERP handles the “what,” your shop floor equipment handles the “how.” An MES connects directly to the systems that control your machinery, like SCADA and PLCs. It sends specific work instructions, recipes, and operational parameters right to the machines, telling them exactly what to do and when. In return, the machines and sensors feed a constant stream of real-time data back to the MES. This includes cycle times, machine status, and any alerts or alarms. With the rise of the Industrial Internet of Things (IIoT), MES can also connect to smart sensors across your facility, giving you an even richer layer of data for machine monitoring and performance analysis.
Understanding the Data Flow
The MES acts as the central hub for all your manufacturing data, creating a single source of truth for your operations. It pulls information from your ERP (the production plan), your machines and sensors (the real-time status), and your operators (quality checks and manual inputs). The system then organizes and contextualizes all this raw data, transforming it into clear, actionable insights. This creates a powerful feedback loop. The ERP knows exactly what’s been produced, your production managers can see bottlenecks as they happen, and your operators have the clear instructions they need. This comprehensive approach to shop floor data collection ensures that your entire operation is synchronized and responsive.
What Are the Benefits of Implementing an MES?
Putting a Manufacturing Execution System in place is about more than just adding new software—it’s about transforming how your shop floor runs. An MES gives you a clear, real-time view of your entire production process, from start to finish. This visibility allows you to move from reactive problem-solving to proactive management. Instead of putting out fires, you can prevent them from starting. By connecting your machines, materials, and people, an MES helps you streamline operations, enforce quality, and make smarter decisions based on solid data, not just guesswork. Let’s look at the specific ways an MES can make a real difference in your facility.
Increase Operational Efficiency and OEE
An MES brings order to the natural chaos of a busy shop floor. It centralizes all critical production information, making it easier to coordinate tasks and keep everything moving smoothly. With a clear view of every work order and machine status, you can optimize your production scheduling to make the best use of your resources. This system helps you understand your production capacity better, identify bottlenecks before they cause delays, and ultimately produce more with less waste. It’s a direct path to improving your Overall Equipment Effectiveness (OEE) by ensuring your machines and teams are working as efficiently as possible.
Improve Product Quality and Compliance
Maintaining high product quality is non-negotiable, and an MES acts as your digital quality control manager. It enforces your quality standards by integrating checks and data collection points directly into the manufacturing process. This creates a detailed digital record, or an “as-built” history, for every single product that leaves your floor. This level of traceability is essential for industries with strict regulatory requirements, like aerospace or medical devices. By automating shop floor data collection, you can catch deviations early, reduce rework, and ensure every part meets exact specifications.
Make Better Decisions with Real-Time Data
One of the most powerful features of an MES is its ability to deliver real-time information. Instead of waiting for end-of-shift reports, you get a live look at what’s happening on the floor right now. This immediate feedback loop allows you to spot issues the moment they arise, from a machine that’s running slow to a potential quality problem. With access to accurate, up-to-the-minute data analytics, your managers can make quick, informed decisions that keep production on track and prevent small hiccups from turning into major disruptions.
Reduce Downtime and Waste
Unplanned downtime and material waste can quietly eat away at your profits. An MES helps you fight back on both fronts. By continuously monitoring machine performance, it can help you identify the root causes of downtime, allowing you to shift from reactive repairs to a more predictive maintenance schedule. At the same time, by optimizing production flow and improving quality control, an MES significantly reduces scrap and rework. These efficiencies lead to direct cost savings and a more sustainable operation, which you can see in the results shared in our case studies.
Preparing for MES Implementation Challenges
Let’s be honest: implementing any new system is a major project, and an MES is no exception. It’s a significant investment of time, money, and effort. But knowing what to expect can make the entire process smoother and far more successful. Instead of seeing these points as roadblocks, think of them as a checklist to help you prepare. By planning for these common challenges, you can set your team and your shop up for a seamless transition.
The biggest hurdles usually fall into a few key areas: the technical complexity of the system itself, getting your team on board with the change, and managing the budget and customization process. With a solid plan, you can address each of these head-on and ensure your MES implementation delivers the results you’re looking for. The goal is to find a partner who understands these challenges and can guide you through them, turning potential problems into opportunities for improvement.
Tackling System Complexity and Integration
An MES isn’t a simple app you download and run. Setting it up takes careful planning and customization to fit your unique operations. One of the most common challenges is getting the MES to integrate with your existing software, especially your ERP. You need these systems to share data smoothly to get a complete picture of your business, but making that connection can be tricky. This is where a lot of projects can get delayed or go over budget. It’s crucial to map out exactly how the MES will connect with your other systems before you begin, ensuring the data flows correctly from the front office to the shop floor and back again.
Guiding Your Team Through the Change
Technology is only one part of the equation; your people are the other. A new MES will change daily workflows, and its success depends entirely on your team’s adoption. If your company culture already struggles with poor communication or trust issues, a new system can unfortunately magnify those problems. Before you implement an MES, focus on improving communication between departments. Define clear processes for how planning and production will work together using the new tools. This isn’t just about installing software—it’s about building a more connected and collaborative operational culture from the ground up.
Overcoming Resistance and Communication Gaps
It’s human nature to resist change. Your team is used to doing things a certain way, and a new system can feel disruptive. That’s why clear communication and thorough training are non-negotiable. Your team needs to understand why this change is happening and how it will make their jobs easier in the long run. One great strategy is to start daily morning meetings with supervisors and managers to review schedules and talk through any issues. This creates an open forum for questions and support, helping everyone feel involved in the process. Finding a true partner for your implementation, not just a vendor, can make all the difference in supporting your team.
Planning for Customization and Costs
The cost of an MES can vary widely depending on the complexity of your operations, how many other systems it needs to connect with, and the number of facilities you have. Think of an MES as a powerful but empty framework. It needs to be configured and tailored to your specific workflows, products, and machines. This customization requires expert knowledge and is a significant part of the overall investment. Before you commit, work with a provider to clearly define your shop’s needs and get a realistic understanding of the total cost, including setup and training. A good first step is to request a demo to see how the system can be adapted to your environment.
Must-Have Features in an MES
Not all MES platforms are created equal. When you’re evaluating your options, it’s easy to get lost in a long list of features. To cut through the noise, focus on the core capabilities that will actually make a difference on your shop floor. A modern MES should be more than just a data repository; it should be a dynamic tool that helps you make smarter, faster decisions. Think of these features as the non-negotiables—the foundational elements that will support your team and drive real growth. From seeing your operations in real-time to predicting future maintenance needs, these are the features that separate a basic system from a truly transformative one.
Real-Time Data and Analytics
The ability to see what’s happening on your shop floor right now is the most critical feature of any MES. You can’t fix problems you don’t know exist. A strong MES connects directly to your equipment to provide a live feed of production data. This allows you to monitor performance, track resource use, and watch key metrics like Overall Equipment Effectiveness (OEE) as they happen. With accurate, up-to-the-minute information, you can spot bottlenecks, address downtime immediately, and get a true picture of your shop’s efficiency. This continuous flow of information is the foundation for all other improvements, turning raw numbers into actionable data analytics.
Custom Dashboards and Reports
Raw data is useful, but it’s not very user-friendly. The best MES solutions translate complex information into clear, visual formats. Look for a system that offers customizable dashboards and reports. Your plant manager needs to see different information than your CEO, and your system should adapt to that. Easy-to-understand charts and graphs help everyone on your team quickly identify trends, track progress against goals, and make informed decisions without needing to be a data scientist. This visual approach makes it simple to monitor machines and share production results across the entire organization, ensuring everyone is on the same page.
Mobile and Cloud Access
Your work doesn’t stop when you step away from your desk, and your MES shouldn’t either. Modern manufacturing requires flexibility, which is why mobile and cloud access are essential. A cloud-based MES means your team can access critical data from anywhere with an internet connection—whether they’re on the shop floor with a tablet or checking in from home. This creates a single source of truth that is always accessible, improving collaboration and enabling faster responses to urgent issues. It breaks down information silos and ensures that decision-makers have the data they need, whenever they need it.
AI and Machine Learning Features
Artificial intelligence is no longer a futuristic concept; it’s a practical tool for manufacturing. An MES with AI and machine learning capabilities can take your operations to the next level. These smart systems can analyze data to predict when a machine might need maintenance, helping you prevent costly breakdowns before they happen. They can also optimize production schedules on the fly, adjusting for unexpected changes to keep things running smoothly. This move toward smarter analysis helps you get more from your data, driving continuous improvement and making your entire production process more resilient and efficient.
How to Measure the Success of Your MES
Implementing a Manufacturing Execution System is a significant investment of time and resources, so you’ll want to know it’s actually paying off. Success isn’t just a gut feeling that things are running smoother; it’s about seeing clear, measurable improvements in your operations. The right MES provides insight-rich analytics that turn raw shop floor data into a clear story of your progress. By tracking the right metrics, you can prove the system’s value, justify the investment, and identify new opportunities for growth.
Measuring success starts with establishing a baseline. Before you go live, capture data on your current performance across key areas. How long does a typical job take? What’s your average downtime per shift? What’s your on-time delivery rate? With these benchmarks in place, you can track changes over time and see exactly how your MES is moving the needle. This data-driven approach takes the guesswork out of evaluating your new system and gives you concrete evidence of its impact on your bottom line.
Key Performance Indicators (KPIs) to Watch
Key Performance Indicators (KPIs) are the vital signs of your manufacturing operations. They are specific, measurable values that show how effectively you’re achieving your main business objectives. Instead of getting lost in a sea of data, focusing on a few core KPIs helps you see what truly matters. One of the most important is Overall Equipment Effectiveness (OEE), which measures how well your machines are utilized by combining availability, performance, and quality into a single score.
Other critical KPIs to monitor include machine downtime, cycle time, and labor productivity. An effective MES makes this easy by providing real-time machine monitoring and automatically collecting the data you need. By watching these numbers, you can quickly spot bottlenecks, understand production loss, and see how efficiently your team is working. These insights allow you to make targeted improvements that have a direct impact on your shop’s performance.
Tracking Production and Quality Metrics
Beyond how your machines are running, you need to measure the results of your production process. This means tracking metrics related to output and quality. Key metrics here include yield, which is the percentage of non-defective products you produce, and scrap rate. A successful MES implementation should lead to a higher yield and less waste, as you gain better control over your processes and can catch issues before they become major problems.
Effective production scheduling also plays a huge role in your output. You should track metrics like on-time delivery rate and schedule attainment to see if you’re meeting customer deadlines and sticking to your plan. An MES gives you the visibility to see how jobs are progressing against the schedule, allowing you to make adjustments on the fly. Consistently hitting your production targets without sacrificing quality is a clear sign your system is working.
Analyzing ROI and Cost Reduction
Ultimately, the success of your MES comes down to its financial impact. Calculating the return on investment (ROI) is how you connect operational improvements to bottom-line results. Start by looking at cost reductions. By minimizing downtime, reducing scrap, and optimizing labor, your MES directly lowers your cost per unit. Tracking these savings over time will help you build a strong case for the system’s value.
Increased throughput is another major component of ROI. When your machines run more efficiently and your schedule is optimized, you can produce more in the same amount of time, opening the door to take on more work without adding equipment or staff. By combining cost savings with revenue gains from increased capacity, you can paint a full picture of your MES’s financial benefits. Reviewing customer success stories can also provide a helpful benchmark for what to expect.
MES vs. Other Manufacturing Software
The world of manufacturing software is full of acronyms, and it’s easy to get them mixed up. You’ve probably heard of ERPs and maybe even SCADA systems. So, where does an MES fit in? Think of it less as a competition and more as a team. Each system has a specific job, and they work best when they work together. Let’s clear up the confusion and look at how an MES compares to other common software, so you can see exactly what it brings to the table.
MES vs. ERP: What’s the Difference?
This is one of the most common questions, and for good reason. An Enterprise Resource Planning (ERP) system is like the central command center for your entire business. It handles the big-picture stuff: finance, human resources, sales, and supply chain management. It knows what needs to be made and when, but it doesn’t have visibility into how it’s being made on the shop floor. That’s where the MES comes in. An MES is the on-the-ground manager, focused exclusively on the factory floor. It takes the high-level plans from the ERP and turns them into actionable tasks, tracking every step of the production process in real time. They’re two sides of the same coin, with the ERP handling business logistics and the MES managing factory operations.
MES vs. SCADA: Which Do You Need?
Now let’s go a level deeper, right down to the machines themselves. A SCADA (Supervisory Control and Data Acquisition) system is all about real-time control and data collection directly from your industrial equipment. It’s the system that lets you monitor pressures, temperatures, and cycle times. While SCADA is great at collecting raw data, an MES provides the context. It takes that raw data and connects it to work orders, operator schedules, and quality specs. So, while SCADA tells you a machine stopped, the MES can tell you why it stopped, who was operating it, and how it impacts your overall production scheduling. You don’t choose one over the other; an MES works with SCADA to create a complete picture of shop floor performance.
When an MES Is the Right Choice
So, how do you know if you need an MES? If you’re struggling with inefficiencies, high scrap rates, or a general lack of visibility into what’s happening on the floor, an MES is likely the answer. It’s for the plant manager who can’t get accurate production counts until the end of a shift or the team that has trouble tracking down why a specific batch failed quality control. By providing real-time insights, an MES helps you spot problems as they happen, not after the fact. If you feel like you’re making decisions based on outdated information or guesswork, implementing an MES can bring clarity and control, leading to significant long-term savings and operational improvements. You can see how other shops have made this work by looking at a few case studies.
How to Choose the Right MES for Your Shop
Picking a Manufacturing Execution System is a major decision, and it’s easy to get overwhelmed by flashy demos and long feature lists. The key isn’t finding the “best” MES on the market, but finding the one that’s the right fit for your shop, your team, and your specific challenges. A system that works wonders for one facility might be a clunky, expensive paperweight for another.
The process comes down to three core steps: understanding what you truly need, finding a vendor who acts like a partner, and planning a smart, phased rollout. Taking the time to get these steps right will make the difference between a smooth transition that improves your bottom line and a frustrating implementation that creates more problems than it solves. Let’s walk through how to approach each one.
Define Your Shop’s Needs
Before you even think about scheduling a software demo, take a step back and look at your current processes. If you’re not already using them, try mapping your workflow with simple visual tools like a T-card board or a Kanban system. This exercise forces you to get crystal clear on how work actually moves through your shop, often revealing bottlenecks and inefficiencies you didn’t know you had. Once you have that clear picture, you can start asking the right questions.
What are your biggest pain points right now? Is it unpredictable downtime? Inaccurate job costing? Or maybe the constant struggle of manual data entry? Pinpoint the specific problems you need to solve. This will help you create a must-have feature list, whether that’s real-time production scheduling to manage capacity or detailed analytics to track performance.
Evaluate Vendor Support and Capabilities
When you evaluate an MES provider, you’re not just buying software; you’re starting a long-term relationship. Look for a partner who is invested in your success, not just in making a sale. A critical question to ask is how much control you’ll have over the system post-installation. You want a system that your team can learn to maintain and adapt themselves, so you aren’t stuck paying for a service call every time you need a minor adjustment.
Think about the future, too. Your shop’s needs will evolve, and your MES should be able to grow with you. Does the system integrate with newer technologies that align with Industry 4.0 principles? A flexible, forward-thinking platform will serve you far better than a rigid one. Finally, don’t underestimate the value of great training and support. The most powerful software in the world is useless if your team doesn’t know how to use it effectively.
Plan Your Implementation
A successful MES implementation is as much about people as it is about technology. One of the biggest mistakes companies make is trying to do too much, too soon. Instead, plan a phased rollout. Start with the features that address your most pressing needs. This approach allows your team to adapt to the new system gradually, and it helps you score some early wins that build momentum and get everyone on board.
It’s also crucial to be honest about your company culture. An MES is a tool for transparency, and if there are underlying issues with communication or trust, the software can amplify them. Involve your team from the very beginning, from the operators on the floor to the managers in the office. When people feel like they are part of the process, they are far more likely to embrace the change and help make it a success. You can see how other shops have managed this by looking at different case studies.
Related Articles
- No ERP Required: 3 Benefits of a Standalone MES for Job Shops
- 5 top things to look for in a scheduling and analytics system
- How do I know if I need a Scheduling (MES) system versus an ERP?
- The Manufacturing Tool ERP Consultants Need to Close Their Sale
- Why Machine Monitoring Is the Missing Link in Your Production Scheduling
Frequently Asked Questions
Is my shop too small for an MES? This is a common question, and the answer has less to do with your company’s size and more to do with its complexity. If you’re struggling to track jobs, manage schedules, or get a clear picture of what’s happening on the floor, an MES can help. Modern systems are highly scalable, so you don’t need to be a massive enterprise to benefit. The right system can be tailored to solve your specific problems, whether you have five machines or fifty.
What’s the difference between an MES and the production scheduling software we already use? Think of production scheduling as one important chapter in a much larger book. Your scheduling software is excellent at planning who does what and when. A Manufacturing Execution System does that, but it also manages the entire story of production. It tracks the real-time progress of those scheduled jobs, monitors machine performance, enforces quality checks, and traces materials from start to finish, giving you a live, complete view of your operations.
Our ERP system has a manufacturing module. Isn’t that enough? While an ERP’s manufacturing module is great for handling the business side of production—like inventory and orders—it doesn’t have a direct, live connection to your shop floor. It knows what you plan to make, but it doesn’t know what’s actually happening with your machines and operators right now. An MES is the essential bridge that provides that real-time data, feeding accurate production details back to the ERP so your business plan always reflects reality.
Do my operators need to be tech experts to use this system? Not at all. A well-designed MES should make your team’s job easier, not more complicated. The goal is to provide operators with clear, simple instructions and intuitive tools to record their progress. The interface should be straightforward, often using touch screens and simple menus. The system handles the complex data collection in the background, allowing your team to focus on what they do best: making high-quality products.
How long does a typical MES implementation take? The timeline can vary quite a bit depending on the complexity of your shop and how many systems need to be connected. However, a smart implementation isn’t about speed; it’s about a smooth transition. Many shops find success with a phased approach, starting with the features that solve their biggest pain points first. This allows your team to adapt gradually and lets you see a return on your investment much sooner.